
Profiles, tapers and hardened material that a cutter cannot touch, cut with a wire and no cutting force.
Wire EDM cuts with electricity instead of an edge. A thin brass wire erodes a path through conductive material, so the part sees no cutting force, no tool pressure and no distortion worth speaking of. You need it when the material is already hardened, when a profile has sharp inside corners or a taper that no end mill can produce, when a punch has to match a die, or when the feature is simply tighter than a milled or ground surface will reliably hold.
The department runs five Agie wire machines: the Progress V3 with a 19.77 by 13.77 by 16 inch envelope, the Progress VP3, the Progress 2 and Progress VP2, and a Classic 2S. Beside them sit two Mitsubishi sinker EDMs, the EA8 and the EA8PV, for cavities and blind features, and a Charmilles HD20 hole shooter for start holes through hardened stock. Programs come from OptiCam, written for wire from the start rather than adapted from a milling path.
Wire runs unattended. A job loaded at the end of the day is finished in the morning, which is what lets a hardened tooling part or a batch of gears fit a schedule that a manual process never could.
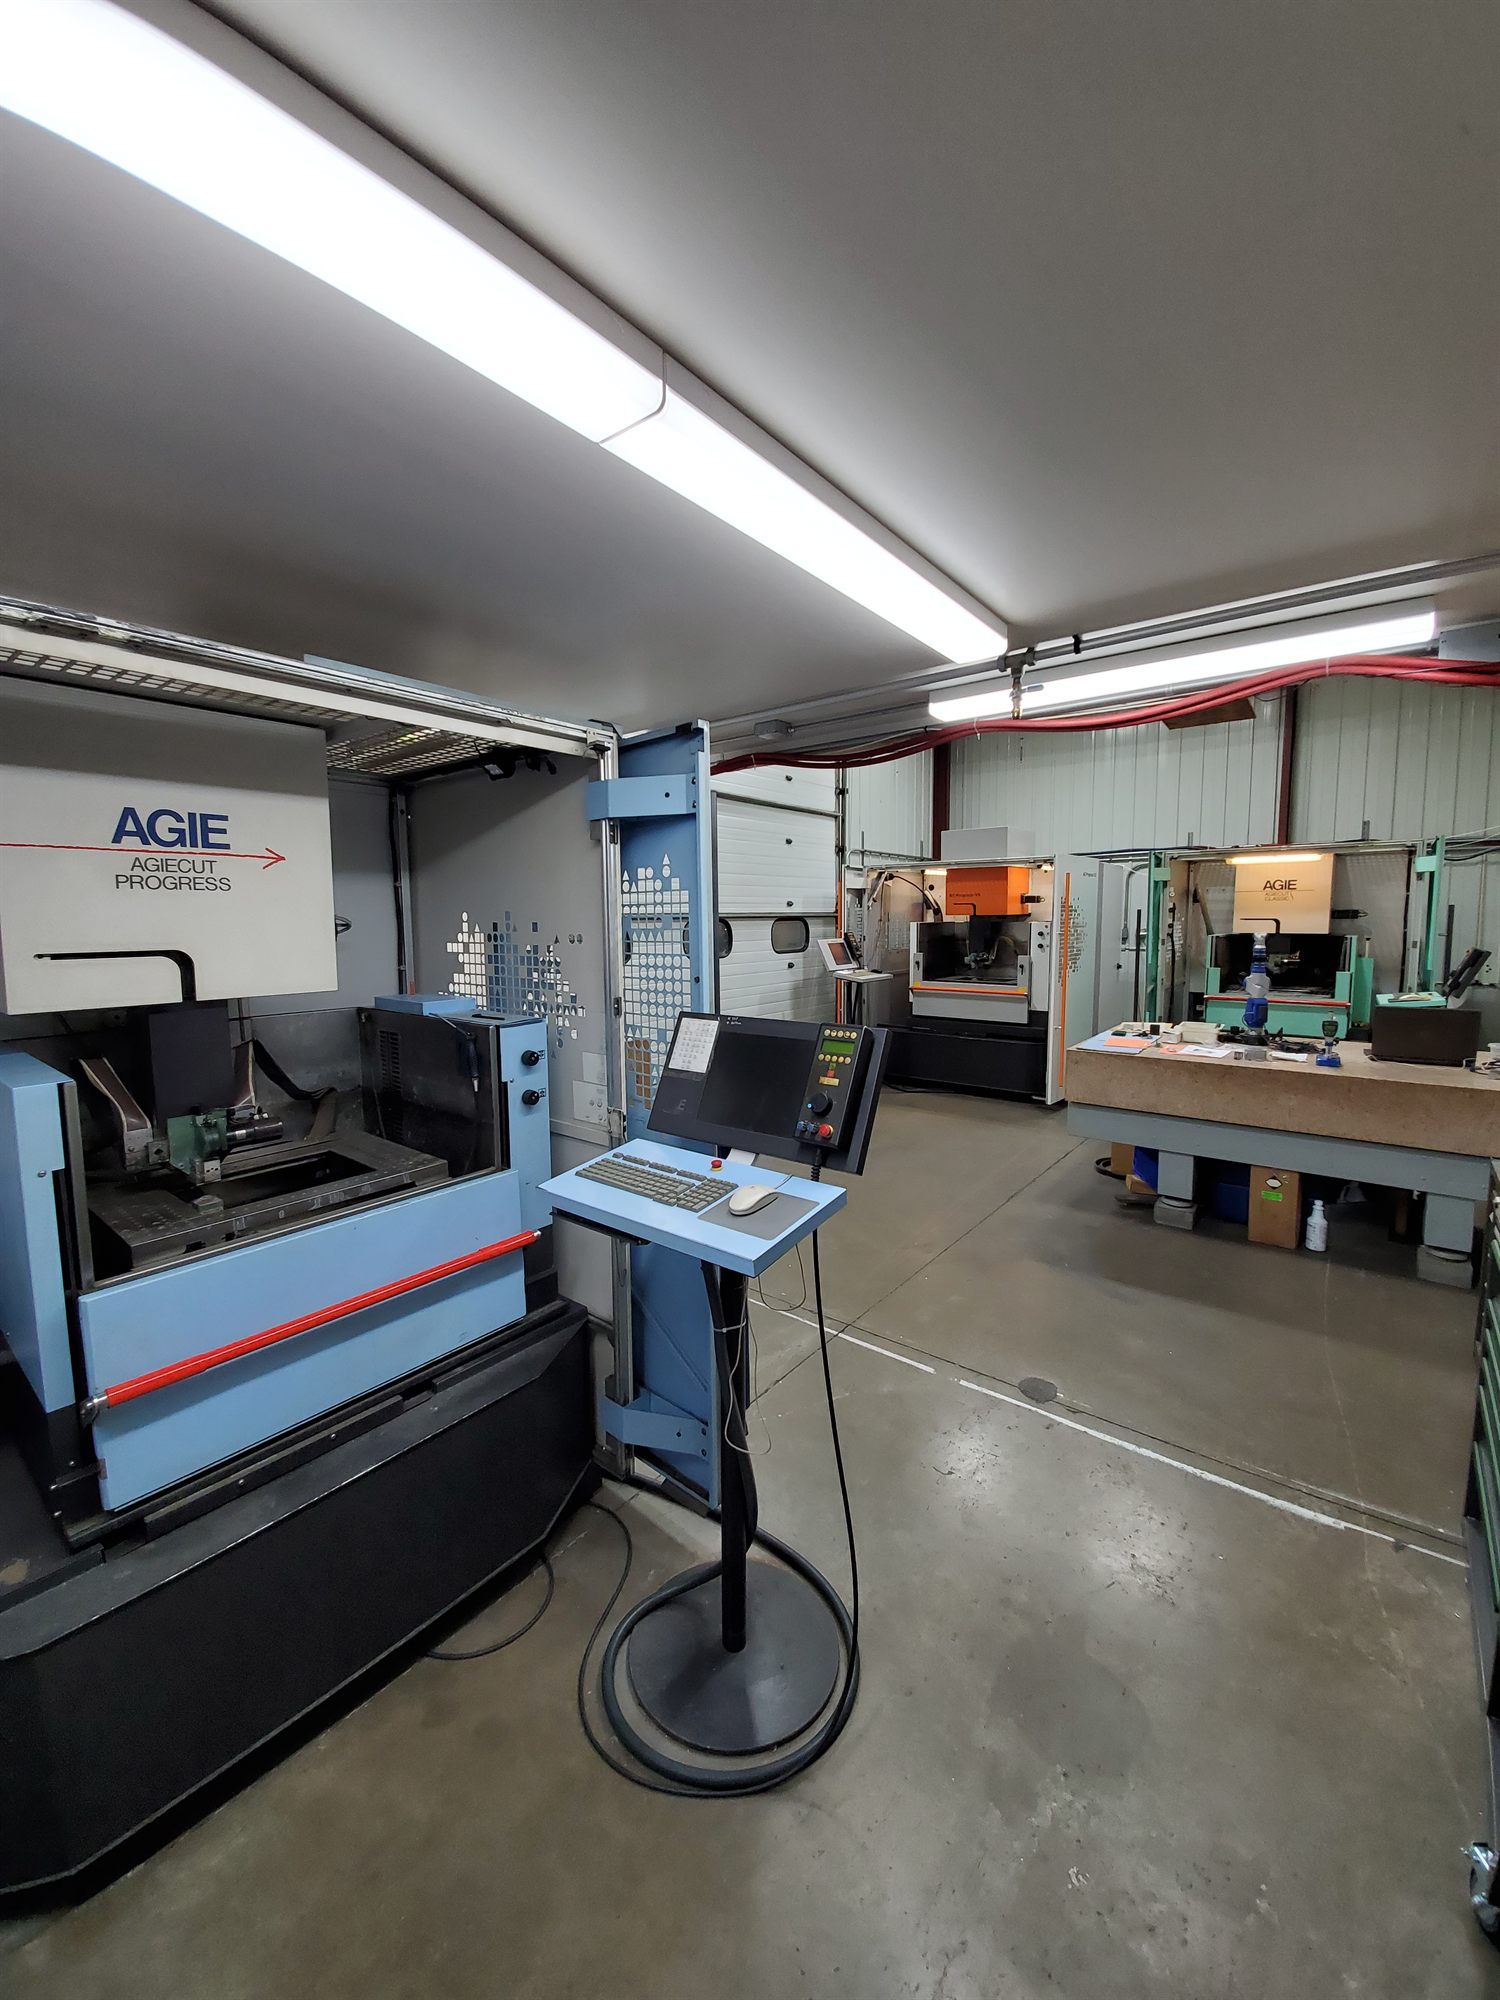
Pulled from the full equipment list, with travels and capacities as they stand on the floor today.
Hardened tool steels, stainless, titanium and other conductive alloys, including parts that have already been heat treated in our own ovens. Wire cuts at finished hardness, so the sequence can be heat treat first and cut second, with no distortion to chase afterward.
Wire EDM is the process to specify when a profile or a fit is tighter than the rest of the part. Because the wire never touches the work, the accuracy comes from the machine and the program rather than from tool wear, and it holds from the first part to the last in the batch. Profiles are verified on the Wenzel CMM and the Gauge Master 21 inch comparator, and the inspection is recorded against the print. See quality and traceability.
Upload a drawing, tell us the quantity and the material, and we'll come back with a quote and a realistic date. Not an optimistic one.