
Shafts, bushings, fittings and turned production parts, from bar feed to one-off housings.
Turning makes round parts, and it makes them fast. Shafts, pins, bushings, fittings, spacers, anything with a centerline. You need it when the print is mostly diameters and lengths, when concentricity between features matters, or when the quantity calls for bar-fed production that runs while nobody is standing at the machine.
Our Mazak QuickTurn Nexus lathes carry sub-spindles and live tooling, which means a part can be turned, cross-drilled, milled flat and parted off complete, front and back, in a single cycle. Three-inch bar feeders keep them running through a shift. For small-diameter work the Citizen L16 and Tsugami SS20 Swiss screw machines hold bar to 16 and 20 millimeters and turn out long, slender or intricate parts that a conventional lathe would chatter on.
Manual lathes with digital readouts are still here for the one-piece repair job or the quick modification that does not justify a program.
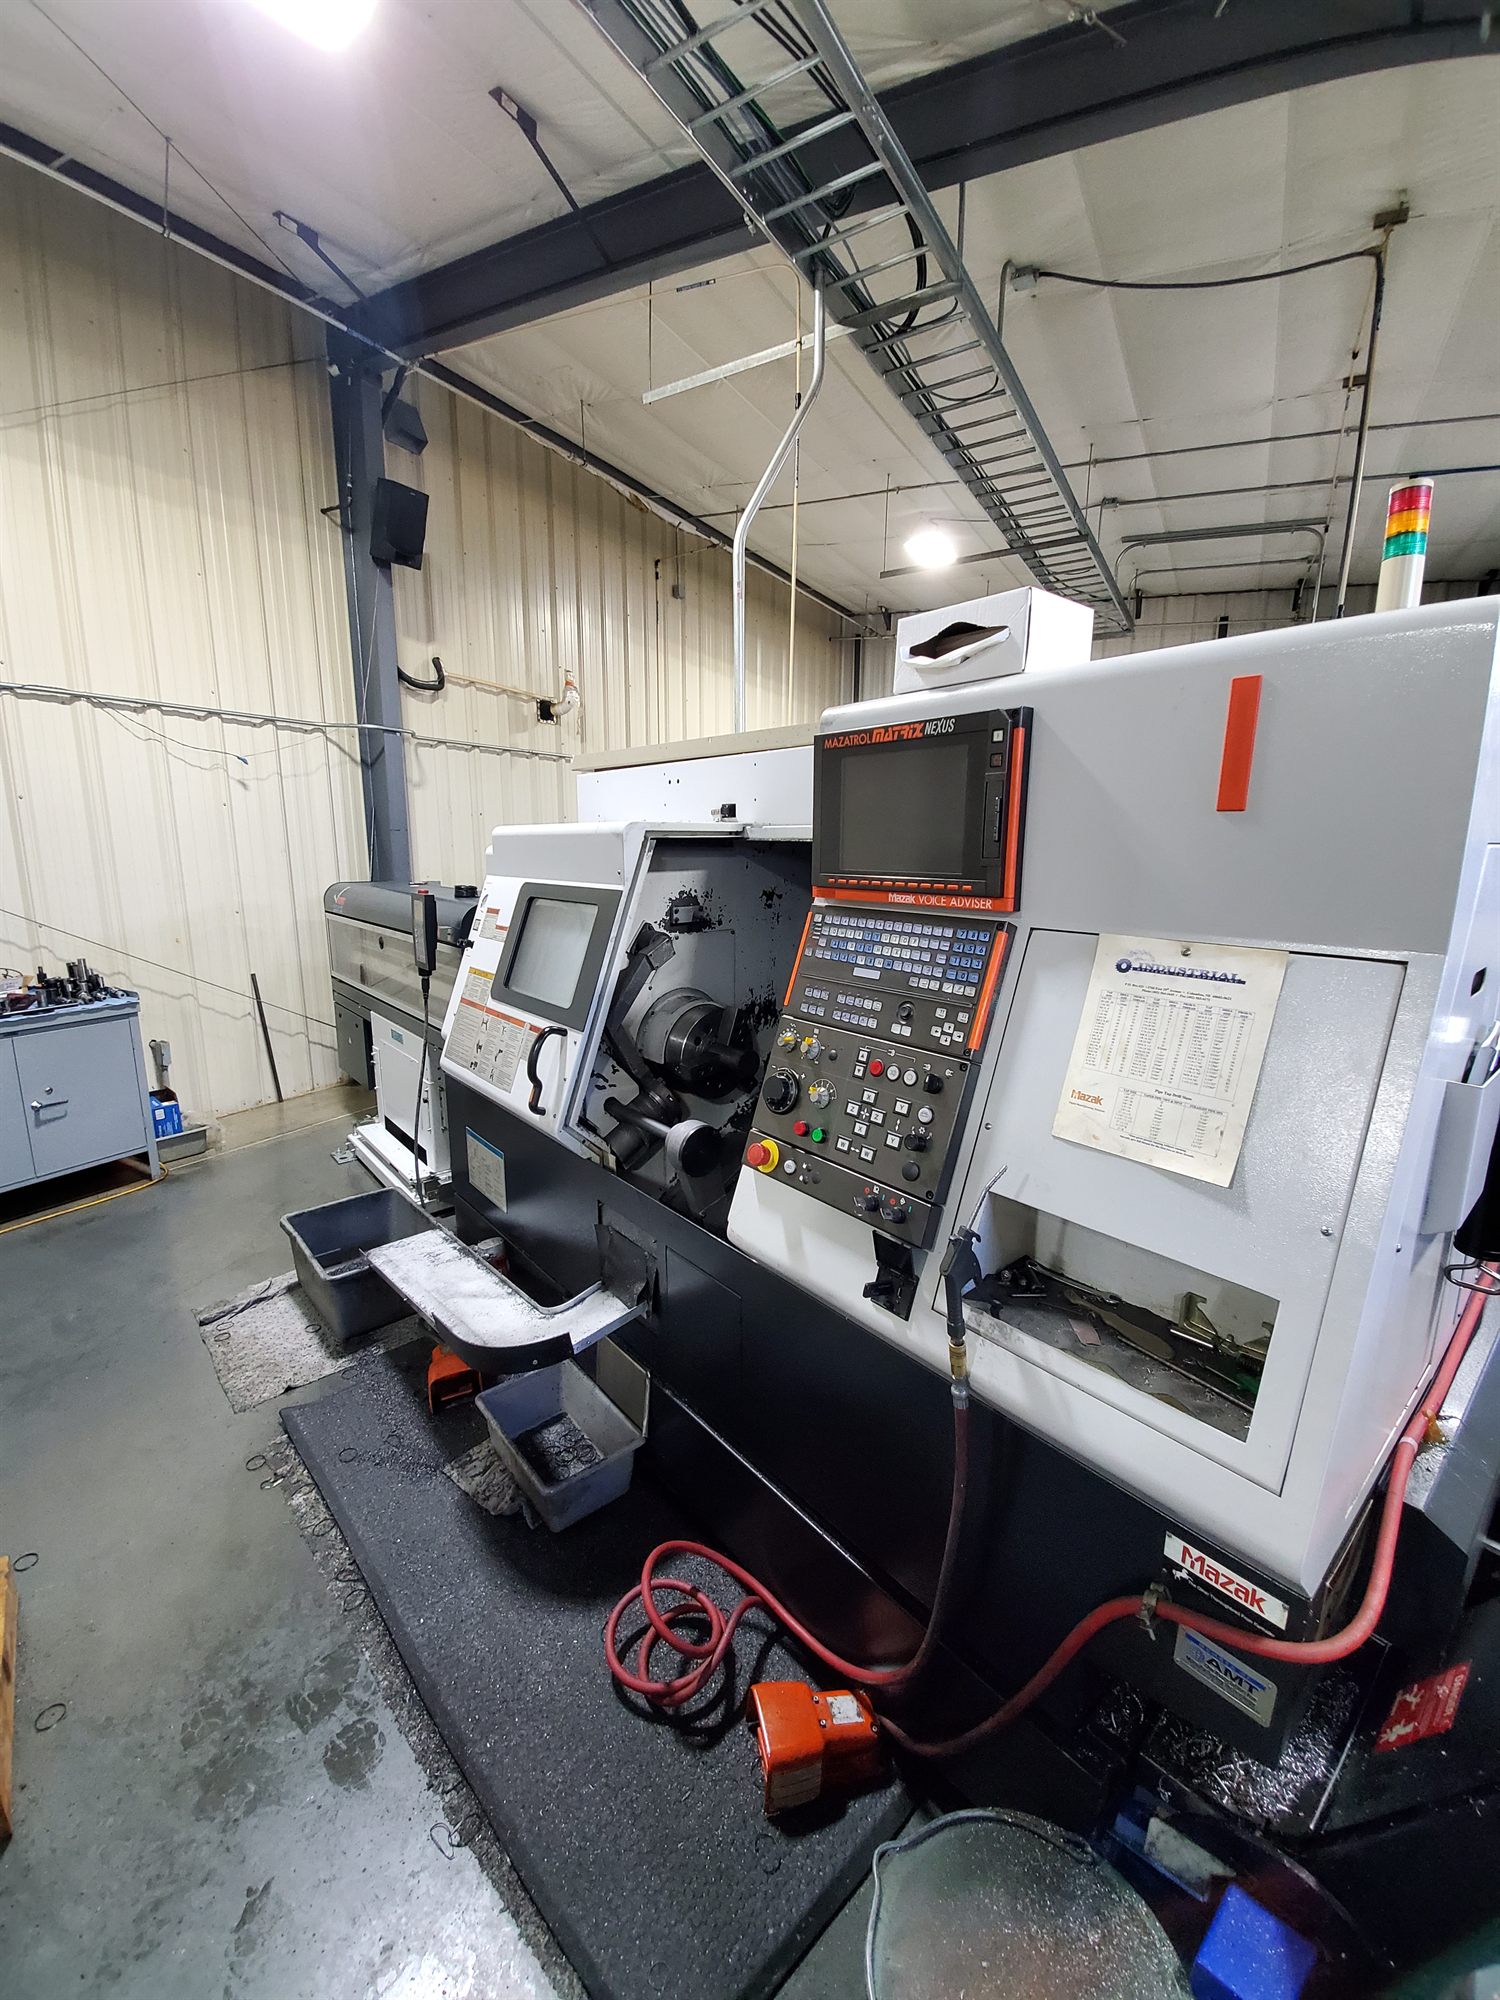
Pulled from the full equipment list, with travels and capacities as they stand on the floor today.
Steel and alloy bar, stainless, aluminum, brass, bronze and titanium, in bar stock to three inches on the Mazaks and to 20 millimeters on the Swiss machines. Larger blanks, castings and forgings are chucked on the 22 by 40 inch machines.
Turned diameters, runout and concentricity are checked on the Wenzel five-axis CMM and with the gauge, pin and thread gauge inventory, and every job carries documented in-process and final inspection. Send the print with the tolerances marked and we quote against them. The detail is on the quality page.
Upload a drawing, tell us the quantity and the material, and we'll come back with a quote and a realistic date. Not an optimistic one.